China Top 10 Factors Affecting CNC Machine Performance?

Time:2026-10-01 Author:Sophia
0%

CNC machine performance is shaped by more than spindle speed or controller brand. In Chinese factories, a small thermal shift can move a machined hole beyond tolerance. Tool wear, vibration, coolant condition, lubrication, programming quality, material behavior, fixture rigidity, operator skill, maintenance, and factory environment all matter. This article examines the China top 10 factors affecting CNC machine performance through practical production evidence and engineering standards. The central question is simple: what factors affect cnc machine performance?

Deloitte’s 2024 Smart Manufacturing and Operations Survey shows that manufacturers increasingly connect equipment data with maintenance and process decisions. Yet digital monitoring cannot correct a poorly aligned spindle or an unstable fixture. The World Economic Forum’s Global Lighthouse Network has reported major gains in productivity and quality from connected manufacturing, but those results depend on disciplined implementation, not software alone. ISO 230 standards also emphasize measurement accuracy, positioning performance, and machine-tool testing, giving engineers a reliable framework for evaluation. These sources support a balanced view: data helps, but mechanical fundamentals remain decisive.

On a real shop floor, performance may decline after a warm-up cycle, a coolant change, or a batch-material variation. That detail is easy to miss. Maintenance teams sometimes blame the machine too quickly, while programmers may overlook cutting-force changes. The ten factors below combine measurable indicators with practical experience from machining operations in China. Some conclusions remain imperfect, because machine age, workload, supplier quality, and operator habits differ widely. That uncertainty deserves attention, not convenient assumptions.
China Top 10 Factors Affecting CNC Machine Performance?

CNC Machine Performance in China: Key Evaluation Factors

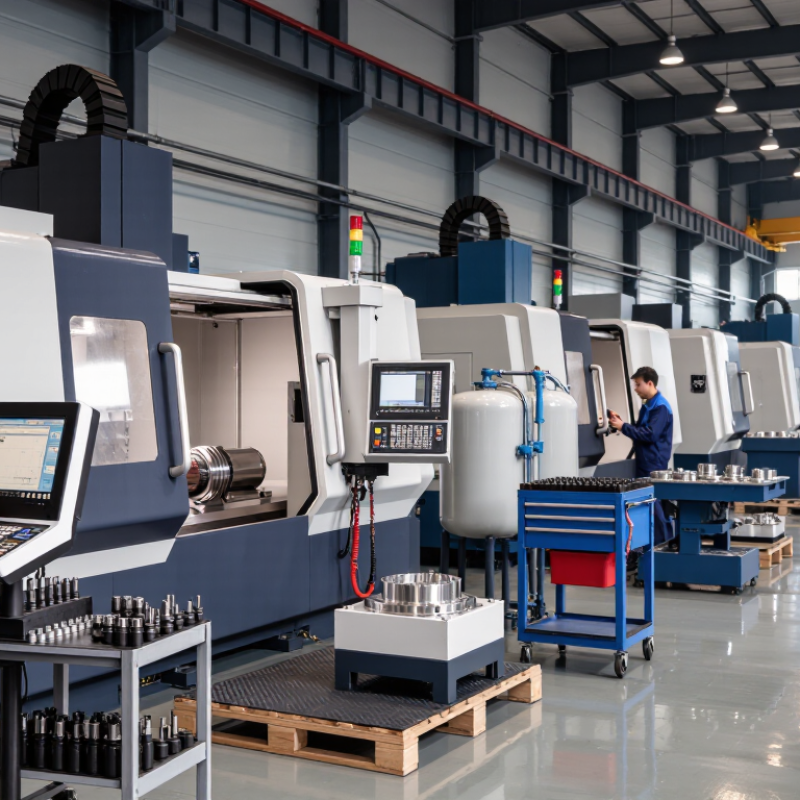
Evaluating CNC machine performance in China requires more than reading speed and accuracy figures. In factory visits, I look at repeatability after long cutting cycles, not only the first test piece. A stable machine should hold dimensions when spindle heat rises and coolant conditions change. Thermal drift often appears quietly. Inspectors should record measurements at different times of day. This exposes weaknesses that polished demonstrations can hide.

Mechanical rigidity is equally important. Heavy cuts should not create chatter, poor surface finish, or sudden tool wear. Spindle runout, axis backlash, guideway condition, and clamping strength deserve direct inspection. The control system must respond smoothly, while electrical cabinets need clean wiring and practical cooling. Small details matter. Poor cable routing can become expensive downtime.

China’s production environment also adds local considerations. Check power stability, workshop temperature, dust control, coolant management, and technician training. Ask for maintenance records and verify calibration with traceable instruments. Supplier documentation should match measured results, not promises. Cost remains important, but the cheapest purchase can demand more service later. No scorecard is perfect. Some evaluations still miss operator habits, setup quality, and rushed maintenance. These human factors can change performance more than a brochure suggests.

Machine Design, Rigidity, and Mechanical Accuracy

China Top 10 Factors Affecting CNC Machine Performance?

Machine design sets the foundation for stable CNC performance. A heavy, well-ribbed base reduces vibration during cutting. Frame rigidity matters when tools remove hard materials at high speed. Weak structures can create chatter, poor finishes, and uneven tool wear. Spindle accuracy depends on bearing quality, preload, balance, and thermal control. Linear guides and ball screws must resist deflection under changing loads. Precise alignment is essential. Even a small installation error can affect hole position across a large workpiece.

Mechanical accuracy also depends on lubrication, calibration, temperature, and assembly consistency. In practical workshops, operators often check axis backlash, spindle runout, and repeatability before trusting production data. A clean way cover protects moving parts from chips and dust. However, protection alone cannot repair poor design. Thermal expansion remains difficult, especially during long machining cycles. Coolant temperature, room conditions, and warm-up procedures influence final dimensions. Control software can compensate for some errors, but compensation is not a substitute for rigidity. I have seen accurate measurements change after several hours of cutting. That result deserves investigation, not excuses. Maintenance records, inspection tools, and operator experience complete the accuracy chain. Some designs still prioritize speed over stiffness, and that trade-off should be questioned.

China CNC Machine Performance: Top 10 Influencing Factors

Relative Engineering Impact Index (0–100)

Machine rigidity, mechanical accuracy, thermal stability, and spindle performance generally have the greatest influence on CNC machining results. The index is a comparative engineering reference based on how strongly each factor can affect dimensional accuracy, surface finish, vibration, productivity, and process consistency. Actual results depend on machine configuration, workpiece material, tooling, cutting parameters, and maintenance.

Spindle Systems, Drives, and Motion Control

In Chinese CNC workshops, spindle performance often decides surface quality before cutting data does. A spindle may reach high speed, yet still produce chatter, heat, or uneven finishes. Bearing preload, lubrication, cooling stability, and tool-holder balance require regular inspection. Even a small runout error can leave visible marks on an aluminum panel. Technicians should record temperature changes during warm-up, not only listen for abnormal noise. A quiet spindle can still hide problems.

The spindle drive controls torque, speed response, and energy use under changing loads. Incorrect acceleration settings may cause vibration when the tool enters hard material. Motion-control tuning also affects contour accuracy, especially during small-radius machining. Servo gain, encoder feedback, backlash, and axis alignment must work together. Poor cable connections can create intermittent feedback errors. These faults waste hours.

Real shop experience shows that clean data matters. Operators should compare commanded speed with actual speed, then review current, position error, and cutting results. Environmental heat can shift machine geometry during long production runs. Stable coolant temperature helps, but it is not a complete solution. I have seen teams replace mechanical parts before checking drive parameters. That mistake is expensive. Maintenance records should include tool wear, spindle temperature, vibration, and recent program changes. Some settings still need practical trials, because a theoretically correct adjustment may behave differently on each machine.

Cutting Tools, Workholding, and Machining Parameters

Cutting tools, workholding, and machining parameters strongly influence CNC machine performance in China’s diverse production environments. A sharp tool reduces cutting force, heat, and burr formation. Tool geometry must match the material, wall thickness, and required surface finish. For example, a small end mill can deflect during deep pocketing, even when the machine appears rigid. I have seen operators blame machine accuracy when tool wear caused the real problem.

Workholding controls stability from the first cut. A vise, fixture, or vacuum setup should support the part near the cutting zone. Excessive clamping pressure can deform thin aluminum or stainless-steel components. Insufficient pressure allows vibration and shifting. Clean contact surfaces matter. One metal chip can tilt a workpiece slightly. That small error may ruin a tight-tolerance feature. I once assumed a damaged fixture was acceptable, and the setup produced inconsistent dimensions.

Machining parameters must be tested as a system. Spindle speed, feed rate, cutting depth, and coolant flow affect one another. Increasing speed without adjusting feed can create heat and premature tool failure. A conservative trial cut reveals vibration before full production begins. Operators should inspect chips, listen for chatter, and measure the first completed part. Cutting data from another machine may not transfer perfectly. Material batches, tool overhang, and fixture stiffness can change the result. Sometimes a slower cycle produces better reliability. That tradeoff deserves careful review.

China Top 10 Factors Affecting CNC Machine Performance? - Cutting Tools, Workholding, and Machining Parameters

No. Performance Factor Key Variables Typical Effect on Performance Practical Control Indicators Recommended Practice
1 Cutting Tool Geometry and Condition Rake angle, clearance angle, edge preparation, tool wear, chipping, and built-up edge Directly affects cutting force, surface finish, dimensional accuracy, heat generation, and tool life Flank wear, cutting-edge damage, burr formation, vibration, and changes in spindle load Inspect tools at planned intervals and replace or recondition them before wear causes dimensional drift
2 Cutting Tool Material and Coating Carbide grade, ceramic or high-speed steel selection, coating type, hot hardness, and toughness Determines allowable cutting speed, resistance to abrasion and thermal wear, and stability during interrupted cuts Tool-life trend, edge wear pattern, workpiece material, hardness, and cutting temperature Match tool grade and coating to the workpiece material, cutting speed, coolant method, and interruption level
3 Workholding Rigidity and Clamping Clamping force, contact area, fixture stiffness, jaw condition, locating accuracy, and unsupported overhang Insufficient rigidity causes chatter, workpiece movement, taper, poor repeatability, and possible damage to the fixture or tool Part displacement, witness marks, vibration, runout, and variation between repeated setups Minimize tool and workpiece overhang, use clean locating surfaces, and apply controlled, consistent clamping force
4 Spindle and Axis Accuracy Spindle runout, bearing condition, axis backlash, positioning accuracy, repeatability, and geometric alignment Influences hole size, circularity, contour accuracy, tool life, and consistency across multiple parts Runout measurement, ball-bar or laser-test results, backlash checks, and dimensional inspection data Perform scheduled calibration, alignment checks, spindle inspections, and preventive maintenance
5 Cutting Speed, Feed, and Depth of Cut Spindle speed, feed per tooth or revolution, axial depth, radial width, chip load, and material removal rate Incorrect parameters increase cutting forces, heat, cycle time, tool wear, chatter, or poor surface finish Spindle-load percentage, chip form, tool temperature, vibration, surface roughness, and cycle time Use tool and material data as a starting point, then adjust parameters using measured load, wear, and finish results
6 Workpiece Material and Condition Hardness, tensile strength, microstructure, heat treatment, residual stress, casting skin, and stock allowance Changes cutting force, tool wear mechanism, chip formation, dimensional stability, and achievable productivity Material certification, hardness testing, stock variation, chip shape, and changes in spindle load Verify material condition before machining and separate parameter plans for soft, hardened, abrasive, or work-hardening materials
7 Coolant and Chip Evacuation Coolant concentration, flow rate, pressure, temperature, filtration, nozzle position, and chip removal Poor cooling or chip evacuation increases thermal damage, recutting, surface defects, tool wear, and machine contamination Coolant concentration, visible chip accumulation, fluid temperature, odor, foam, and surface discoloration Maintain the specified fluid concentration, direct coolant at the cutting zone, and clear chips before they are recut
8 Toolpath and Programming Quality Entry and exit motion, cornering, acceleration, smoothing, step-over, feed transitions, and collision avoidance Affects cycle time, sudden load changes, contour accuracy, surface finish, and risk of tool breakage Motion smoothness, feed-rate variation, corner marks, cycle-time data, and simulated tool clearance Use smooth engagement strategies, avoid abrupt direction changes, and verify programs through simulation and dry runs
9 Machine Thermal Stability Ambient temperature, spindle heat, axis motor heat, warm-up time, coolant temperature, and machine operating duration Thermal growth can shift work coordinates, alter hole location, and cause dimensional changes during long production runs First-piece versus later-piece dimensions, spindle temperature, room temperature, and drift over time Use a consistent warm-up routine, stabilize the shop environment, and apply thermal compensation where available
10 Maintenance, Measurement, and Operator Control Lubrication, filter condition, tool offsets, probing, inspection frequency, operator setup, and process documentation Poor maintenance and inconsistent setup increase downtime, scrap rate, dimensional variation, and unexpected failures Overall equipment effectiveness, unplanned downtime, first-pass yield, offset corrections, and inspection records Follow preventive-maintenance schedules, standardize setup procedures, verify offsets, and use closed-loop inspection when practical

Software, Automation, Maintenance, and Operator Skills

CNC machine performance depends heavily on software quality, automation design, maintenance discipline, and operator skills. In daily production, a stable program reduces sudden pauses and inconsistent finishes. A clear toolpath also limits unnecessary movement and cutting heat. Yet software settings can still be wrong. Small errors matter. Operators should verify feed rates, tool offsets, and work coordinates before cutting. Simulation catches many collisions, but simulation is not proof. Real cutting forces can expose weaknesses that screens cannot show.

Automation improves repeatability when sensors, probing systems, and tool measurement work correctly. Automatic tool measurement can detect wear before a finished part fails inspection. However, automation can hide developing problems. I have seen operators trust a sensor while a loose fixture caused vibration. A backup manual check is worth the minute. Production data should be reviewed regularly, not collected and forgotten.

Maintenance protects accuracy over long operating hours. Clean coolant, stable lubrication, and accurate calibration support consistent results. One missed lubrication cycle may create heat, noise, or premature wear. Operator skill remains equally important. Experienced machinists notice unusual sounds, rough chips, and changing spindle loads. Training should include setup practice, alarm interpretation, and safe measurement habits. Admitting uncertainty is useful. A fast cycle is not always a good cycle.

FAQS

How does machine design affect CNC machining performance?

A heavy, ribbed base reduces vibration during cutting. Weak frames can cause chatter, rough surfaces, and uneven tool wear. Speed alone cannot fix poor stiffness.

Why are spindle accuracy and thermal control important?

Bearing preload, balance, lubrication, and cooling influence spindle accuracy. Small runout can leave visible marks on an aluminum panel. A quiet spindle may still hide problems.

How can temperature change machining dimensions?

Long cutting cycles create heat and thermal expansion. Coolant temperature, room conditions, and warm-up procedures affect final dimensions. Measurements may change after several hours.

What should operators inspect before trusting production data?

Check axis backlash, spindle runout, repeatability, and alignment. Record spindle temperature during warm-up. Small installation errors can shift hole positions across a large workpiece.

How do motion settings influence cutting results?

Acceleration, servo gain, encoder feedback, and backlash affect contour accuracy. Incorrect acceleration may create vibration when entering hard material. Theoretical settings still need practical trials.

Can software compensation replace mechanical accuracy?

No. Software can compensate for some errors, but it cannot replace rigidity or accurate assembly. Simulation helps detect collisions, but real cutting forces may reveal hidden weaknesses.

How does automation support consistent production?

Probing, tool measurement, and sensors improve repeatability when they work correctly. Automatic measurement can detect tool wear early. A manual check still matters.

Which maintenance habits protect CNC accuracy?

Keep coolant clean, maintain lubrication, and calibrate axes regularly. Inspect way covers for chips and dust. One missed lubrication cycle can cause heat, noise, or premature wear.

What role does operator experience play in machine performance?

Skilled operators notice unusual sounds, rough chips, and changing spindle loads. They verify tool offsets, feed rates, and work coordinates. Admitting uncertainty is useful. A fast cycle is not always a good cycle.

Conclusion

CNC machine performance in China depends on a combination of design quality, operating conditions, and production management. Key evaluation factors include the machine’s structural rigidity, mechanical accuracy, thermal stability, and resistance to vibration. A strong machine design helps maintain precision during heavy cutting, while properly aligned guideways, screws, and tables support consistent positioning. Spindle power, speed stability, drive response, and motion control also influence surface finish, productivity, and dimensional accuracy.

When considering what factors affect cnc machine performance, it is also important to examine cutting tools, workholding systems, machining parameters, software, automation, maintenance, and operator skills. Suitable tools and secure fixtures improve cutting efficiency and reduce errors, while optimized speed, feed, and depth settings protect both the workpiece and machine. Reliable control software and automation can improve repeatability, but regular inspection, lubrication, calibration, and timely maintenance remain essential. Finally, trained operators play a major role in setup, troubleshooting, and achieving stable long-term performance.
Sophia

Sophia

Sophia is a dedicated marketing professional with an exceptional depth of knowledge about her company's products and services. With a keen understanding of market trends and customer needs, she crafts insightful blog posts that not only inform but also engage readers, enriching the company’s online......